 DITAI
Medical equipment housings.
Made to fit the whole device.
Custom thermoformed covers, panels and enclosures for medical equipment. From the first fitted sample to repeat production, we work through the details that affect assembly, cleaning and service access.

The outside of the equipment
has a job to do.
A housing brings the equipment together visually, but its work does not stop there. It must clear the internal modules, meet neighbouring panels, allow routine cleaning and come off when a technician needs access.


Instrument covers & display surrounds
Screen overlap, connector depth and ventilation compete for space behind a compact cover. Give the bezel and the internal mounting arrangement the same attention as the visible outline.
Mobile equipment & cart panels
Access to brakes, castors and service connections belongs in the housing review. A handle or accessory load needs a defined path to its support; it should not be assigned to a cosmetic panel by default.
Large equipment enclosures
Panel division affects how the equipment is built, shipped and repaired. Removable sections can make a large assembly manageable without opening every joint for a routine service task.
This page focuses on equipment housings and exterior components. Photographs show component configurations, not evidence of clinical approval, sterilization validation or suitability for patient contact.
Start with the cleaning method.
Then choose the surface.
“Suitable for hospital use” is not a material specification. The useful starting point is the actual cleaning product, how it is applied and what the housing must still look like and withstand after repeated exposure.
A material can look unchanged and still lose strength.
Chemical exposure and stress can act together. A formed corner or tightened fixing may behave differently from an unstressed sheet sample. Material screening is useful, but it does not replace an assessment of the finished housing.
Include the complete surface system: sheet, colour, paint, printed markings, labels, adhesive and any bonded fittings. A cleaning method that suits one layer may damage another.
Define the exposure
Identify the cleaner or disinfectant, concentration, wet contact time, application method and frequency. If the equipment uses more than one cleaning regime, list them separately. Do not translate a general “alcohol resistant” statement into compatibility with every formulated wipe.
Agree what counts as failure
Cracking is only one concern. Review colour shift, loss of gloss, tackiness, coating damage, label legibility and the condition of loaded attachments. Set acceptance criteria and the exposure programme with the device team before sample testing.
Keep cleaning and sterilization separate
A wipe-clean outer cover is not automatically suitable for steam, chemical immersion or radiation processing. If the component will undergo a reprocessing cycle, specify that cycle and confirm the exact material and finished-part construction against it.

Assembly & service access
A good fit should survive the next service visit.
A sample that fits once is not the whole requirement. The cover should return to its intended position after removal, without pulling on wiring or relying on the technician to force a flexible panel into place.
Locate first, fasten second
Identify the surfaces and features that locate the housing on the chassis. A screw should retain a supported panel rather than correct a misplaced support. Review the frame, brackets, mounting pads and fastening sequence when a seam changes along its length.
Design a real removal route
Check the last screw, the connector latch and the space needed to lift the panel away. A service door may need different hardware from a fixed rear cover. Agree opening frequency and assess the selected fixing arrangement on representative parts.
Check edges, seams and recesses
Consider where cleaning fluid could collect and whether the intended wipe can reach a joint. A visually narrow seam is not necessarily a sealed seam. Gaskets need supported mating surfaces and controlled compression; any ingress claim needs the relevant assembled-enclosure assessment.
Specify the finished part.
Not just the starting sheet.
The mould controls the formed surface. Drawing stretches the sheet. Trimming establishes the openings and edges. The drawing and inspection plan need to distinguish these three things.
Local wall thickness
Draw depth, corner radii and shape influence wall distribution. Name the locations where a minimum finished wall matters, particularly near attachments and exposed edges. A nominal sheet gauge is not a promise of uniform thickness throughout the housing.
Cut-outs & mating features
Display apertures, vents and mounting holes need a common reference to the assembly. Inspect critical features in an agreed support condition. Tightening every dimension can add cost while leaving the actual interface problem unresolved.
Appearance after forming
Texture and reflected light change across a drawn surface. Compare a representative formed sample with neighbouring parts, not only a flat colour chip. Define visible zones, lighting and viewing distance before appearance approval.
Thermoforming design considerations → CNC trimming and openings →
From separate panels
to a consistent assembly.
A family of covers needs shared references: panel position, aperture location, edge condition and finish. These production photographs show the components and assemblies; they do not substitute for project-specific inspection records.


Material decisions belong
with the device requirements.
ABS, PC/ABS and other thermoformable sheet families can be starting points for an enclosure review. Selection depends on the exact grade, gauge, colour and finish—not on the polymer name alone.
Contact with the user or patient
Identify who touches the component, where and for how long, including foreseeable indirect contact. Biological evaluation concerns the finished device and its intended contact conditions. A resin declaration does not establish the suitability of every pigment, coating, adhesive or manufacturing residue.
Electrical and thermal requirements
Clarify whether the cover is cosmetic or has an insulating, fire-enclosure or other protective function. Discuss relevant thickness, openings, proximity to heat and mounting arrangements with the equipment safety team. A material flame rating alone does not establish compliance of medical electrical equipment.
Shielding and ventilation
Conductive coatings require a defined continuity and grounding arrangement across joints. Ventilation must be reviewed with the internal airflow path and cleaning access. Neither a coating specification nor a grille area establishes the finished device’s EMC or thermal performance.
Impact and handling
Identify likely contact points during use, maintenance and shipping. Include actual support conditions when assessing deflection or damage. An enclosure that protects appearance is not automatically a structural guard, lifting point or impact barrier.
The OEM defines the device’s intended use and applicable requirements. Component supply, material information and agreed manufacturing records support that work; they do not replace device-level verification or regulatory approval.
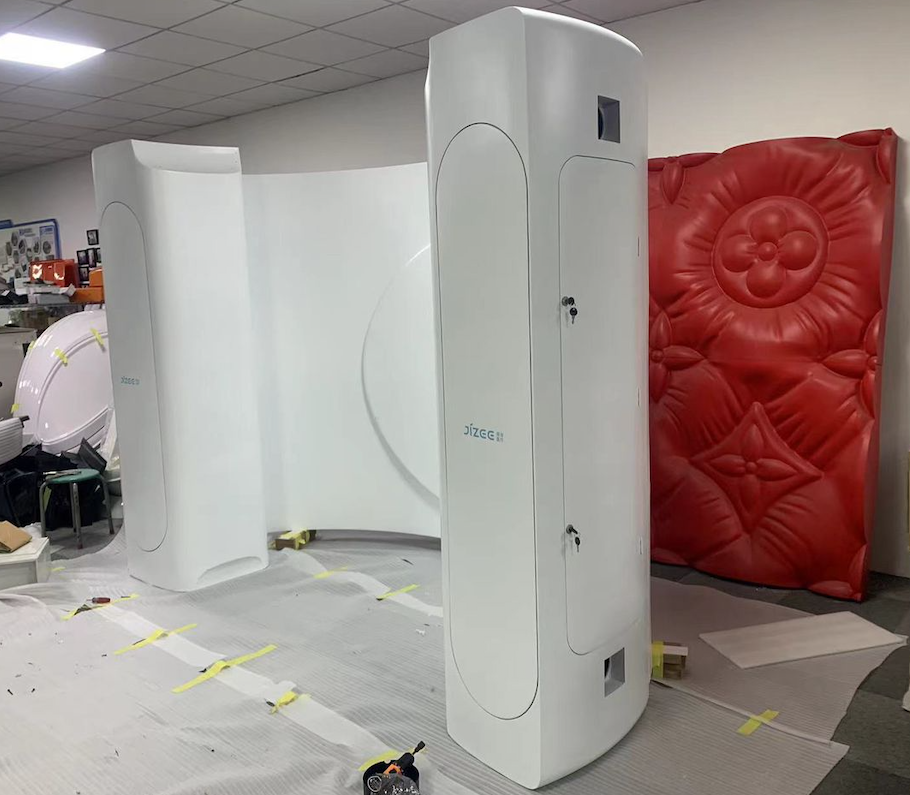
Larger covers need an assembly plan,
not simply a bigger mould.
For a tall or wraparound enclosure, decide where to divide the panels, how they attach and how they are transported. The split line affects tooling, trimming, access and the appearance of the finished equipment.

Know what you are approving.
Keep it identifiable on repeat orders.
Supplier qualification is more useful when the required records are agreed before tooling. Ask for the evidence your quality team actually needs, with the part revision and acceptance method clearly identified.
Material & finish identity
Agree the sheet grade, colour, starting gauge, approved substitutions and certificate requirements. Include coatings and adhesives where used. Define how material and production batches are linked and which records will accompany delivery.
First-article acceptance
Identify the critical dimensions, datums, support condition and appearance reference. Record whether a measurement describes the free part, a fixture-held part or an installed panel. Close open fit issues before treating the sample as a production master.
Changes & deviations
Decide which material, tool, trim-program, finish or attachment changes require customer review. An apparently minor change can affect cleaning compatibility or interchangeability. Record any approved deviation against the affected revision and batch.
Replacement parts & packaging
Consider spare-panel supply alongside the production order. Protect contact faces and visible surfaces without loading a flexible cover out of shape. Agree the identification needed to distinguish similar parts and revisions after they leave the factory.
Questions worth resolving
before the tooling order.
A clear manufacturing boundary is more useful than a broad promise. These are the decisions that shape the quotation and the sample review.
When is thermoforming a sensible route for a medical equipment housing?
It is worth reviewing for relatively large, open-backed covers and panels where tooling investment, part size and production volume matter. Compare the complete finished part: trimming, hardware, painting, assembly and inspection as well as the formed shell. Small enclosed components with numerous integrated bosses or complex snap features may favour another process.
Can a design intended for injection moulding be used unchanged?
Usually it needs a process review. A thermoformed shell does not reproduce solid bosses, ribs or a uniform CAD wall in the same way. Review draft, radii, draw direction, parting lines and secondary fittings before quoting the original geometry as a direct replacement.
Can you guarantee a disinfectant-resistant or sterilizable housing?
Only a defined requirement can be assessed. Provide the exact agents or processing cycle, exposure conditions and acceptance criteria. Grade-specific supplier data can guide selection; representative finished components and the agreed validation programme determine suitability. No universal compatibility claim is made here.
What changes when the housing design is still evolving?
Identify what is released and what remains provisional. A trim-only opening change may be possible without changing the forming tool, but a surface or draw change may not. Material changes also require review of forming, shrinkage, fit and performance; they are not simply a sheet substitution.
Bring the housing.
And what it has to fit.
Send the outer model with the chassis or mating geometry, quantities and intended environment. Mark the important seams, display apertures, mounting features and service panels.
Include the cleaning specification and the records your quality team needs. If those are not settled, tell us what is still open so it can be addressed before tooling.
Tell us about your equipment housing.
Engineering references & scope
These references inform the engineering discussion; they are not certifications of DITAI or the parts pictured.


